No products
Prices are tax included


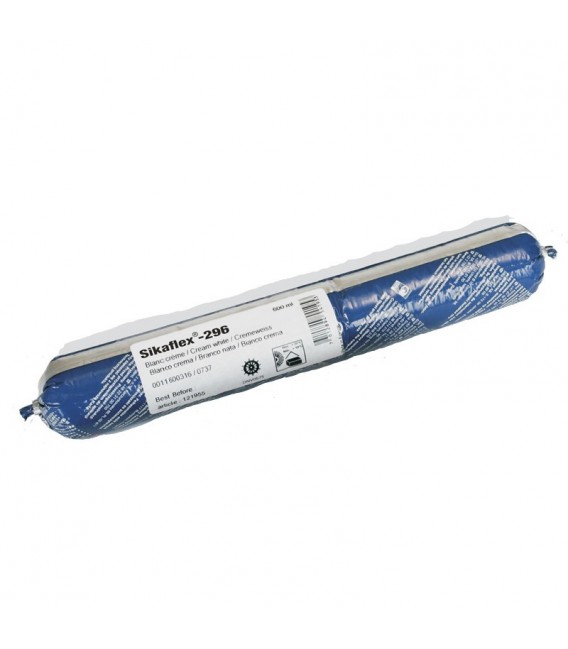
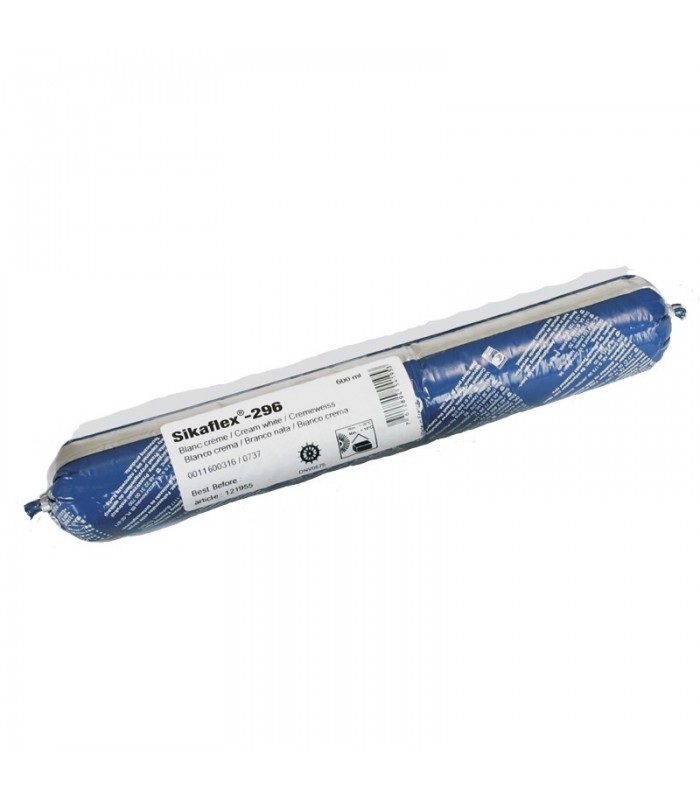
SIKAFLEX® SIKA® 296 UV NERO ML 600
SIKAFLEX® SIKA® 296 UV NERO ML 600
Sikaflex®-296 is a polyurethane adhesive for direct gluing of glass, single-component, elastic, suitable for filling, high-performance polymerizing for exposure to atmospheric moisture. It is suitable for almost all types of application of glass in the shipbuilding industry. Sikaflex®-296 meets the regulations established by the International Maritime Organization (IMO).
Benefits
- Resistant to aging and atmospheric agents
- Excellent work characteristics
- Without solvents and PVC
- Little smell
- Suitable for manual applications and pumping system
- Possible application without primer
- Wheelmark approved
Uses
Sikaflex®-296 is designed for direct glazing applications in shipbuilding and storage markets. It is suitable for use with all kinds of mineral glass windows used in Marine. Before installing laminated protection windows, which incorporate heating elements into the PVB sandwich layer, please contact the Sika Technical Assistance Department for advice. Sikaflex®-296 can be worked with an aesthetic finish and is suitable for visible joints. Ask for advice to the manufacturer and perform tests on original substrates before using Sikaflex®-296 on stress cracking materials. Sikaflex®-296 is only suitable for experienced professionals. Tests with substrates and real conditions must be carried out to ensure adherence and compatibility of materials.
- Chemical base: monocomponent polyurethane
- Color (CQP001-1): Black
- Mechanism of hardening: Polymerization with atmospheric humidity
- Density: 1.2 kg/l
- Tixotropy: Very good
- Application temperature: environment 10 ─ 35 °C
- Skin training time (CQP019-1): 45 minutes A
- Open time (CQP526-1): 30 minutes to
- Hardening speed (CQP049-1): See graph 1
- Volumetric waste (CQP014-1): %
- Coastal hardness A (CQP023-1 /ISO 48-4): 45
- Tensile strength (CQP036-1 / ISO 527): 6 MPa
- Breaking extension (CQP036-1 / ISO 527): 450 %
- Cutting propagation resistance (CQP045-1 / ISO 34): 14 N/mm
- Overlay cutting resistance (CQP046-1 / ISO 4587): 4.5 MPa
- Insulation resistance (CQP079-2 / DIN IEC 60167): 108Ω cm
- Serving temperature (CQP509-1 / CQP513-1): -40 ─ 90 °C
- Stability (CQP016-1): cartridge/unipack 9 months B | barrel/fustin 6 months B
CQP = Corporate Quality Procedures
A) 23 °C / 50 % r. h.
B) storage below 25 °C
APPLICATION
Surface preparation
The surfaces must be clean, dry and free of any trace of fat, oil, dust and contaminants.
Surface treatment depends on the specific nature of the substrates and is essential for a lasting bond. Tips for surface preparation can be found in the current edition of the appropriate Sika® pretreatment table. Consider that these suggestions are based on experience and must in any case be verified by testing on original substrates.
Application
Sikaflex®-296 can be extruded between 10 and 35 ° C (climate and product) but changes in reactivity and application properties must be considered. The optimum temperature for substrate and sealing is between 15 ° C and 25 ° C. Keep in mind the increase in viscosity at low temperature. For easy application, condition the adhesive at room temperature before use. To ensure a uniform thickness of the joint line, it is recommended to apply the adhesive in the form of a triangular cord (see figure 1).
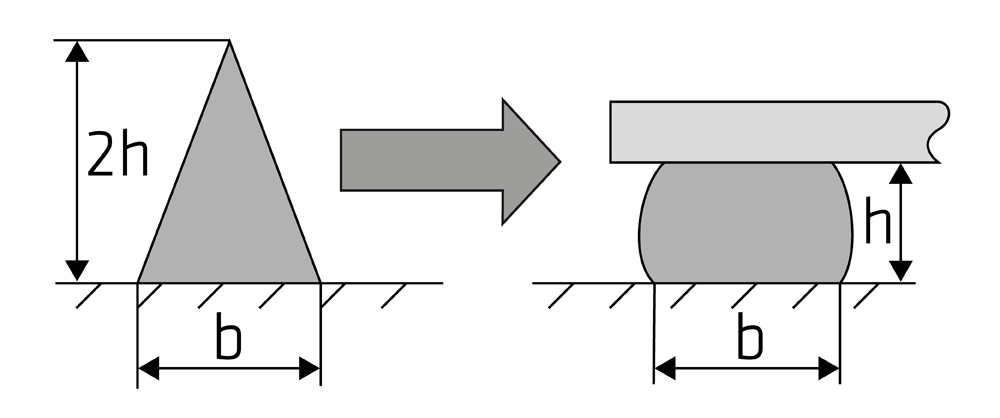
Figure 1: Recommended string configuration
Sikaflex®-296 can be extruded with manual, pneumatic or electrical pistols as well as with pump equipment. Open weather is significantly shorter in the warm and humid climate. The glass must always be installed within the open time. Never join the adhesive parts if the adhesive has built a skin.
For advice on choosing and installing a suitable pumping system, please contact the Sika Industry System Engineering Department.
Brushing and finishing
Tools and finishings must be performed within the skin training time of the product. It is recommended to use Sika® Tooling Agent N. Other finishing agents must be tested for suitability and compatibility before use.
Removal
Non-cured Sikaflex®-296 can be removed from tools and equipment with Sika® Remover-208 or another suitable solvent. Once hardened, the material can only be removed mechanically. The hands and exposed skin must be washed immediately with wipes such as Sika® Cleaner-350H or a suitable industrial hand cleaner and water. Do not use solvents on the skin!